 EN


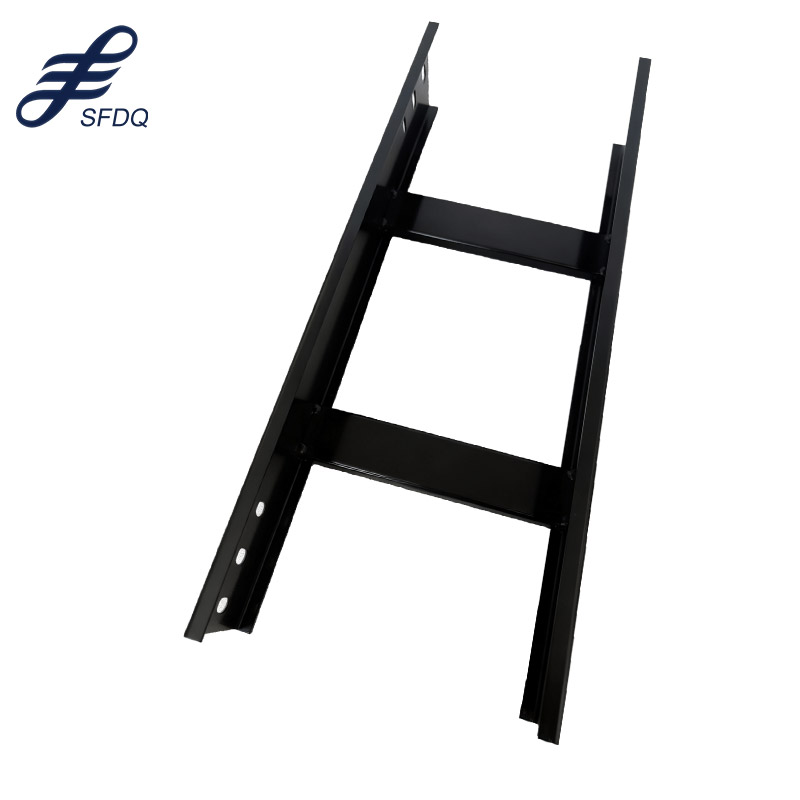
In demanding industrial environments, infrastructure investments must withstand years of operational stress, environmental exposure, and mechanical challenges. The heavy duty cable tray emerges as a critical component for organizations seeking reliable cable management solutions that deliver long-term value. Unlike standard cable trays designed for light to moderate applications, a heavy duty cable tray provides enhanced structural integrity, superior load-bearing capacity, and extended operational life. Understanding the durability advantages of a heavy duty cable tray is essential for facilities managers, plant engineers, and procurement professionals tasked with building resilient infrastructure that minimizes downtime and maximizes return on investment.
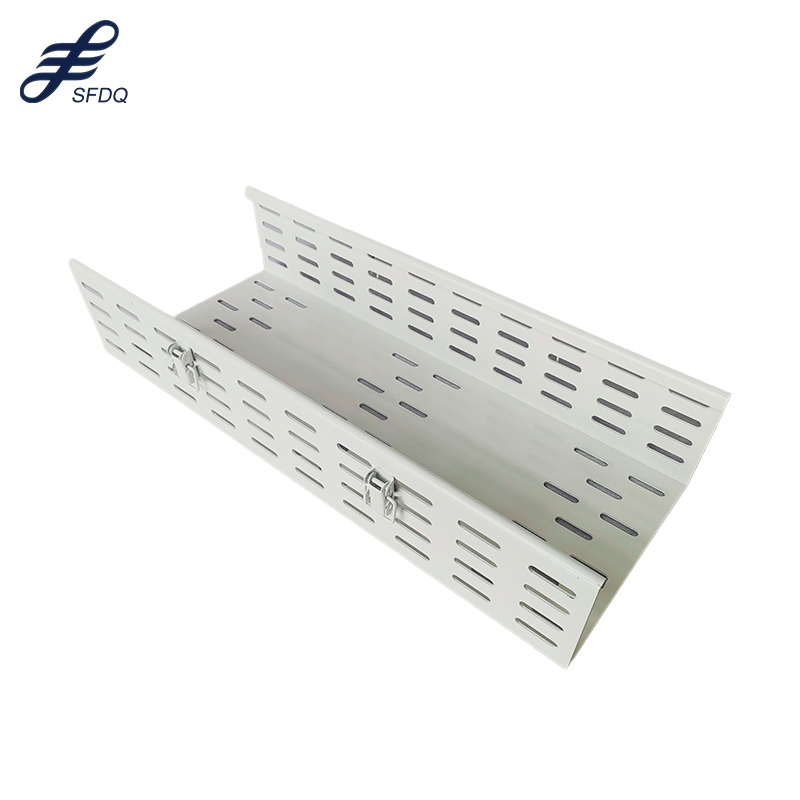
The decision to invest in a heavy duty cable tray represents a strategic commitment to facility performance and operational reliability. Industrial applications ranging from manufacturing plants and data centers to power distribution facilities and petrochemical installations demand cable management systems capable of supporting heavy loads, resisting corrosion, and performing consistently across temperature fluctuations and harsh environments. A heavy duty cable tray addresses these requirements through advanced material selection, reinforced construction methods, and proven durability in real-world conditions. This article explores the tangible durability advantages that make a heavy duty cable tray the preferred choice for mission-critical infrastructure projects.
Superior Load-Bearing Capacity and Structural Strength
Engineering Design for Maximum Performance
The heavy duty cable tray incorporates engineering principles specifically designed to handle substantial cable loads without sagging, deformation, or failure. Traditional cable trays experience deflection under stress, which can compromise cable alignment, create pressure points, and accelerate wear on cable jackets. A heavy duty cable tray utilizes reinforced frame designs, thicker gauge materials, and strategic cross-bracing that distributes loads evenly across the entire structure. The reinforced rungs and sidewalls of a heavy duty cable tray maintain their dimensional stability even when loaded to maximum rated capacity, ensuring cables remain properly supported throughout their service life.
The structural engineering of a heavy duty cable tray typically includes gusseted corner joints, welded connections, and precision-manufactured components that eliminate weak points common in lighter-duty systems. When facilities must support dense cable bundles from multiple systems—power distribution, control signals, telecommunications, and sensor networks—the heavy duty cable tray provides the mechanical foundation necessary for safe and compliant installations. This load-bearing capability prevents the gradual deterioration that occurs when cable trays are over-stressed, extending the operational life of both the tray itself and the cables it supports.
Long-Term Structural Integrity Under Operational Stress
Industrial facilities experience continuous vibration, thermal cycling, and dynamic stress that gradually weakens inadequately designed cable management systems. The heavy duty cable tray resists these degradative forces through its robust construction, which dissipates stress more effectively than standard alternatives. The higher material mass and cross-sectional strength of a heavy duty cable tray means that cyclic loading generates less fatigue stress in individual components, resulting in significantly slower crack initiation and propagation rates. Testing data consistently demonstrates that a heavy duty cable tray maintains structural integrity for decades, whereas lighter systems may require reinforcement or replacement within five to ten years.
The durability advantage of a heavy duty cable tray becomes particularly evident in facilities experiencing high-frequency vibration, such as those adjacent to heavy machinery, compressors, or transportation corridors. The mass and damping characteristics of a heavy duty cable tray naturally absorb vibration energy, protecting both the tray structure and the cables from accelerated wear. In petrochemical plants, manufacturing facilities, and other high-vibration environments, investing in a heavy duty cable tray represents preventive maintenance strategy that reduces emergency repairs and unscheduled downtime.
Material Durability and Corrosion Resistance
Advanced Material Selection for Environmental Protection
Corrosion represents one of the primary causes of premature cable tray failure in industrial and coastal environments. Standard mild steel cable trays succumb to rust and structural degradation within a few years when exposed to moisture, salt spray, or chemical vapors. The heavy duty cable tray typically features materials engineered specifically for corrosion resistance, including aluminum alloy construction, stainless steel options, or steel with advanced protective coatings. These material choices ensure that a heavy duty cable tray maintains structural strength and aesthetic appearance across 15, 20, or even 30-year service intervals, eliminating the need for frequent replacement or costly refurbishment.
Material selection for a heavy duty cable tray goes beyond simple corrosion prevention to include temperature stability and chemical resistance. Facilities in coastal regions, chemical processing plants, and outdoor installations benefit from the proven durability of premium materials integrated into a heavy duty cable tray design. The higher initial investment in material quality delivers exponential cost savings over the system's operational life through reduced maintenance, elimination of emergency repairs, and avoidance of production interruptions caused by cable management failure.
Protective Coating Systems and Surface Treatments
Many heavy duty cable tray systems incorporate multi-layer protective coating systems that provide additional durability beyond the base material properties. Hot-dip galvanizing, powder coating, or specialized epoxy systems create barrier protection that extends the service life of a heavy duty cable tray in aggressive environments. These coating systems are engineered to withstand the rigors of installation, mechanical contact, and environmental exposure without chipping, peeling, or loss of protective function. A properly coated heavy duty cable tray resists corrosion initiation even where mechanical damage has penetrated the surface, providing redundant protection that ensures decades of reliable service.
The investment in protective coating systems for a heavy duty cable tray proves cost-effective when calculated over the full lifecycle. A facility that implements a heavy duty cable tray with premium protective coatings eliminates the recurring maintenance expenses associated with rust treatment, repainting, and partial replacement of corroded sections. In harsh environments, the durability advantage of a properly specified heavy duty cable tray with advanced surface treatments reduces total cost of ownership by 40 to 60 percent compared to standard alternatives requiring frequent maintenance interventions.
Performance Reliability and Reduced Maintenance Requirements
Minimizing Downtime Through Proven Durability
Industrial facilities cannot afford unexpected infrastructure failures that disrupt production schedules, compromise safety protocols, or trigger compliance violations. The heavy duty cable tray delivers performance reliability through conservative engineering, robust materials, and proven field performance across thousands of installations. A heavy duty cable tray designed for the intended application environment eliminates the risk of premature failure that commonly occurs with undersized or inappropriate cable management systems. This reliability translates directly to operational continuity, allowing facility managers to focus on core production rather than emergency repairs to cable management infrastructure.
The durability advantage of a heavy duty cable tray manifests through measurably lower failure rates, extended replacement intervals, and predictable lifecycle costs. Facilities that specify a heavy duty cable tray experience fewer unexpected service calls, reduced inventory requirements for replacement components, and simplified maintenance planning. This operational predictability provides budget certainty and allows maintenance teams to schedule interventions proactively during planned maintenance windows rather than responding to emergency failures.
Lifecycle Cost Analysis and Return on Investment
While the initial purchase price of a heavy duty cable tray may exceed that of standard alternatives, comprehensive lifecycle cost analysis consistently demonstrates superior economic value. A heavy duty cable tray specified for the correct application environment typically delivers 15 to 30 years of service with minimal maintenance, whereas standard systems require replacement or major repairs every 5 to 10 years. When lifecycle costs are calculated including installation labor, maintenance expenses, material costs, and production losses from unplanned downtime, a heavy duty cable tray provides return on investment within 3 to 5 years and continues generating savings throughout its extended operational life.
The durability advantage of a heavy duty cable tray extends beyond financial metrics to include risk mitigation, safety compliance, and operational resilience. Facilities that invest in appropriate cable management infrastructure reduce their exposure to equipment damage, electrical hazards, and regulatory violations. For mission-critical applications where reliability directly impacts revenue and stakeholder trust, the enhanced durability of a heavy duty cable tray represents essential infrastructure investment that protects organizational reputation and operational capability.
FAQ
What makes a heavy duty cable tray different from standard cable trays?
A heavy duty cable tray incorporates reinforced structural design, thicker materials, and advanced protective coatings specifically engineered for demanding industrial environments. Standard cable trays are designed for light to moderate load applications, while a heavy duty cable tray provides increased load capacity, superior corrosion resistance, and extended operational lifespan. The engineering differences include gusseted joints, precision welding, and optimized cross-sectional geometry that distinguishes a heavy duty cable tray from lighter-duty alternatives designed for simpler installations.
How long does a heavy duty cable tray typically last?
A properly specified and installed heavy duty cable tray commonly delivers 20 to 30 years of reliable service in appropriate environmental conditions. The actual service life depends on environmental factors including temperature extremes, moisture exposure, chemical presence, and mechanical stress. When a heavy duty cable tray is selected correctly for the specific application environment and manufactured with premium materials and protective coatings, facilities frequently achieve or exceed 30-year service intervals, making it a highly durable infrastructure investment.
Is a heavy duty cable tray worth the additional upfront investment?
Yes, a heavy duty cable tray provides superior return on investment through reduced maintenance costs, eliminated emergency repairs, extended replacement intervals, and operational reliability. Lifecycle cost analysis typically demonstrates that a heavy duty cable tray recovers its higher initial cost within 3 to 5 years through lower maintenance expenses and avoided production disruptions. For mission-critical facilities where downtime creates significant financial and operational impact, the durability advantage of a heavy duty cable tray justifies the upfront investment as essential infrastructure protection.